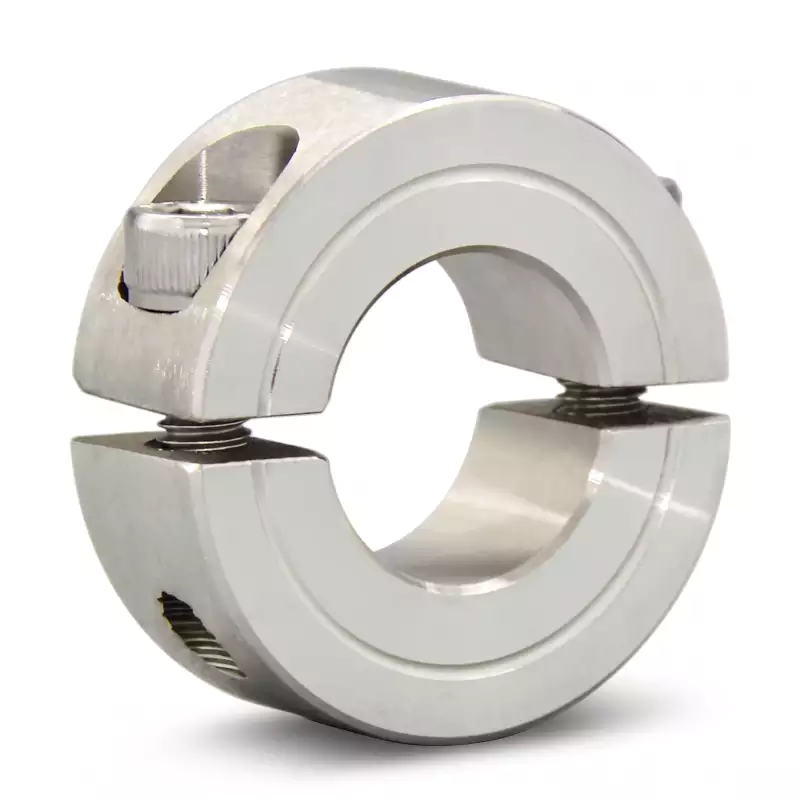
GBC-SCS50 Aluminum Clamp Type Shaft Collar – 50mm Bore
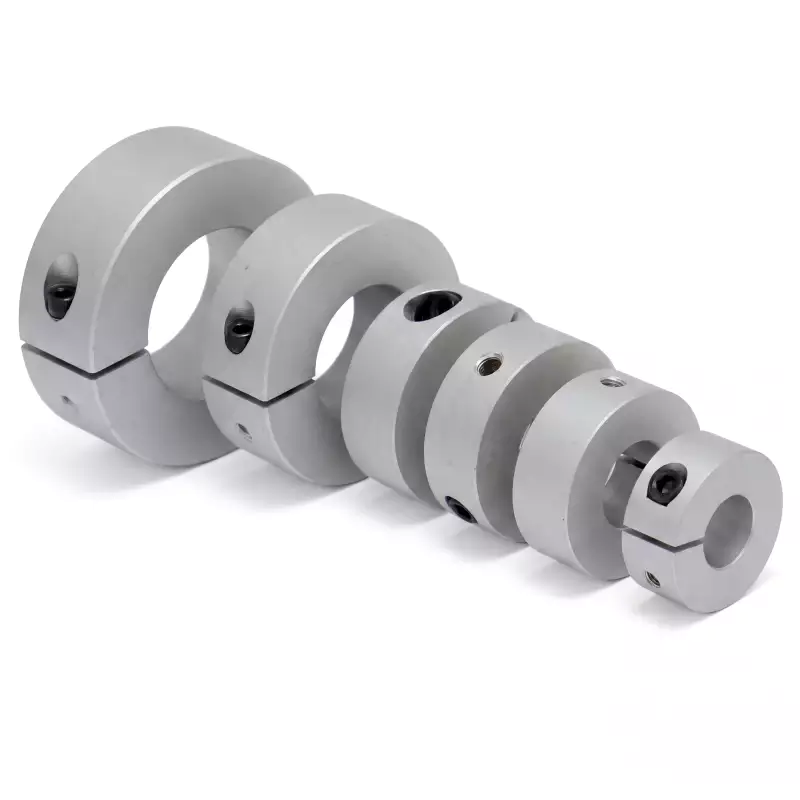
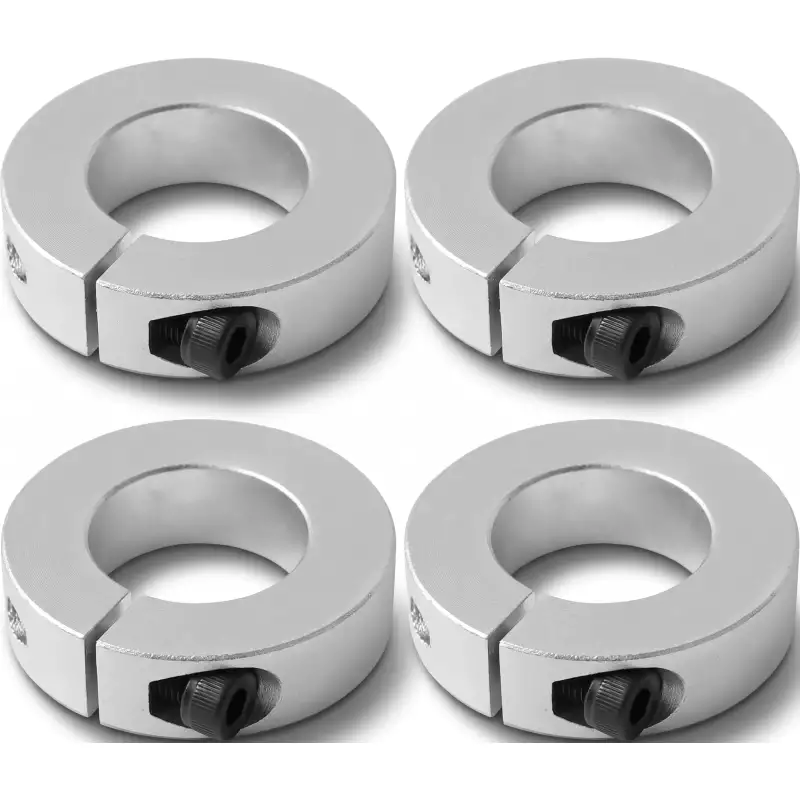
The GBC-SCS50 aluminum clamp-type shaft collar fits 50 mm bore shafts. OD 85 mm, face width 22 mm, M10 screw, 3 mm wide slot for field assembly ease, optional 14 mm keyway. Purpose-built for large industrial pump drive shafts, rolling mill pass-line rollers, and paper machine press-section roll stubs.
MOQ: 50 pcs. Minimum order value USD 1,500; mixed orders and trial quantities welcome.
50mm Bore Aluminum Clamp Shaft Collar – Wide-Slot 3mm Design for Large Industrial Pump & Rolling Mill Auxiliary Shafts
| Parameter | Value | Note |
|---|---|---|
| SKU / Model | GBC-SCS50 | GBC SCS Series — Large Bore |
| Bore Diameter (d) | 50 mm | Shaft h6 tolerance: 50.000 / 49.984 mm |
| Outer Diameter (D) | 85 mm | Provides thick wall for high-clamp loads |
| Face Width (B) | 22 mm | Extended width for high axial bearing area |
| Clamping Screw | M10 socket-head cap screw | Torque: 30–35 N·m · 10 mm hex key |
| Slot Width (W) | 3.0 mm | Wide slot for easy assembly over shaft features |
| Keyway Width (K) | 14 mm | DIN 6885 Form A; plain bore is default supply |
| Recommended Torque | 30–35 N·m | Use calibrated torque wrench |
| Material | Aluminium alloy | Hard-anodize, electroless nickel & steel variants available |
| MOQ | 100 pcs | Custom engineering drawings accepted |
Product Overview
At 50 mm bore, the GBC-SCS50 introduces two significant engineering evolutions simultaneously: the slot width widens from 2 mm to 3 mm, and the OD grows to 85 mm — the widest gap and one of the largest ODs in the SCS aluminium range. The 3 mm slot provides substantially greater radial deflection travel as the M10 screw closes the collar, making it markedly easier to slide the collar over shaft keyways, snap-ring grooves, thread run-outs, and machined flats during field assembly of large shaft assemblies where precision alignment fixtures are not available. For large industrial pump shafts in water-treatment and process-plant installations, rolling-mill pass-line roller shafts in steel and aluminium production, and paper-machine press-section roll shafts in pulp and paper mills, this ease-of-assembly characteristic directly reduces installation time and the risk of bore damage during forced collar seating. The 22 mm face width maintains the high axial bearing area established at SCS45, and the M10 screw continues to deliver clamping torque in the 28–32 N·m range, translating to axial holding forces above 7 kN on ground h6-tolerance shafts — sufficient for the high-sustained-thrust environments of these large-machine applications.
Key Features
Non-Damaging Clamp Design
Circumferential clamping force eliminates shaft surface indentation, preserving ground shaft finishes and protecting adjacent seals and bearings from the accelerated wear caused by the stress-concentration marks that set-screw collars leave on large-diameter shafts where replacement cost is high.
M10 High-Capacity Clamping Screw
The M10 socket-head cap screw delivers clamping torque up to 30–35 N·m — the highest in the SCS range at this bore level — producing axial holding forces that match the sustained thrust loads of large industrial machinery operating continuously at rated capacity.
3.0 mm Wide Slot — Field Assembly Advantage
The 3.0 mm slot width provides generous bore clearance for sliding the collar over shaft keyways, threads, and groove features without tools or force — a significant advantage on large shaft assemblies built in the field without alignment fixtures or heating equipment.
22 mm Face Width — Maximum Axial Bearing Area
The 22 mm face width is matched to the bore and OD at this size to deliver the highest axial bearing area in the SCS range, distributing clamping contact pressure across a wide band that maximises holding force and minimises bore surface pressure under long-term sustained axial loads.
14 mm DIN 6885 Keyway — Full-Torque Locking Option
The 14 mm keyway follows DIN 6885 Form A for 50 mm bore, providing both axial location and full-rated rotational torque transmission through a single component. Specify at order — default supply is plain bore without keyway.
Typical Application Scenarios
Large Industrial Pump Drive Shafts
Horizontal split-case and end-suction centrifugal pumps in water-treatment plants, irrigation systems, and process-fluid transfer services run on 50 mm shafts in sleeve-bearing housings. The SCS50 locates the drive-end coupling hub against the pump bearing lantern, preventing coupling migration under the combined axial thrust of the pump impeller — which can reach 8–12 kN in high-head single-stage pumps — and the axial reaction of the drive shaft coupling.
Rolling Mill Pass-Line Roller Shafts
Entry and exit guide rollers in wire rod and bar rolling mills mount on 50 mm shafts exposed to severe impact loads from bar ends and cobbles. The SCS50 wide-slot design eases collar installation in the confined rolling mill bay where large fixtures are impractical, while the M10 clamping force retains roller axial positions under the high-impulse loads that would cause narrower or lower-clamp collars to migrate and misalign the rolled product.
Paper Machine Press-Section Roll Shafts
Felt-guide and spreader rolls in paper machine press sections operate on 50 mm stub shafts under sustained radial loads from web tension and press nip forces. The SCS50 locates roll-end bearing housings without machined shaft steps — a practical advantage in paper mills where rolls must be frequently changed and shaft re-machining between rolls would unacceptably extend roll-change downtime.
Dimensional Guide & Shaft Fit Specification
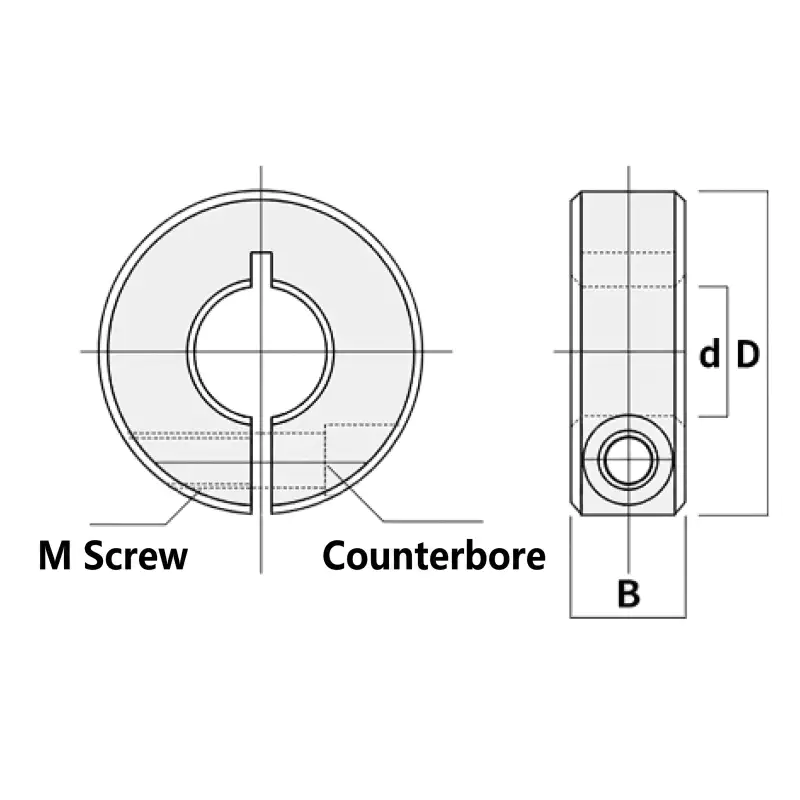
The GBC-SCS50 is defined by bore d = 50 mm, outer diameter D = 85 mm, and face width B = 22 mm. The 3.0 mm slot runs the full face width, providing the radial flex gap that allows the bore to close around the shaft as the M10 screw is tightened to 30–35 N·m. Specify the mating shaft to ISO 286 h6 (50.000 / 49.984 mm) for the optimal pre-installation sliding fit and maximum post-clamping axial retention force. Bore sizes above 40 mm must be verified with a calibrated bore gauge rather than relying on nominal dimensions — manufacturing tolerances on large shafts can approach 0.05 mm and will significantly affect clamping performance if outside the h6 band.
GBC supplies custom configurations including steel and stainless steel construction, extended face widths, twin-screw clamping, marine-grade anodizing, and bore sizes above 60 mm. Contact the GBC team via the enquiry page with your engineering drawing and application details for a tailored quotation.
Model Selection Guide
For 45 mm bore heavy-marine and large-fan applications requiring the same M10 clamping at 2 mm slot, the GBC-SCS45 at 80 mm OD is the predecessor. For the largest shaft size in the SCS aluminium range at 60 mm bore, the GBC-SCS60 steps up to a 95 mm OD and 18 mm keyway for the most demanding heavy-machine main shaft applications.
| Model | Bore | Relation |
|---|---|---|
| GBC-SCS45 | 45mm | ← Smaller |
| GBC-SCS50 | 50 mm | ◀ Current |
| GBC-SCS60 | 60mm | → Larger |
Installation Procedure
- Shaft measurement: Measure the shaft diameter at the collar location using a calibrated micrometer or bore gauge, confirming the dimension falls within ISO h6 (50.000 / 49.984 mm). At large bore sizes, do not assume nominal dimensions — verify physically.
- Surface preparation: Degrease the clamping zone with a solvent wipe. For shafts with light rust or scale, polish with 400-grit abrasive cloth before degreasing. Remove all burrs from keyway edges to prevent bore scoring during collar installation.
- Collar positioning: Open the slot fully by backing off the M10 screw two full turns. Slide the GBC-SCS50 onto the shaft to the required position, referencing a pre-set depth gauge or spacer for repeatable placement. Torque M10 screw to 30–32 N·m using a calibrated torque wrench with an 8 mm hex-bit socket. The 3 mm wide slot allows the collar to be slid over most shaft features without forcing — if resistance is felt, do not hammer the collar; open the slot further by loosening the screw one full turn before re-attempting.
- Torqued clamping: Using a calibrated torque wrench with a 10 mm hex-bit socket, tighten the M10 screw in three steps — 30%, 70%, then 30–35 N·m — checking position after each step. Mark the screw head with a paint pen after final tightening to detect any self-loosening during subsequent inspections.
Frequently Asked Questions
Why does the slot width increase to 3mm at SCS50 versus 2mm at SCS40 and SCS45?
Is the SCS50 suitable as a direct replacement for a machined locating shoulder on a 50mm pump shaft?
What surface treatment is recommended for SCS50 in a paper-mill environment?
Related Products
Browse adjacent sizes and associated shaft components from GBC:
- GBC-SCS45 – 45mm bore aluminum clamp shaft collar — next smaller size in the heavy-bore SCS range
- GBC-SCS60 – 60mm bore aluminum clamp shaft collar — next larger size for maximum axial capacity
- Complete GBC SCS Shaft Collar Series — all standard bore sizes from 6 mm to 60 mm, with custom options beyond
Request a Quote or Discuss a Custom Specification
Minimum order quantity is 100 pcs. GBC supplies steel and stainless steel variants, marine-grade hard-anodizing, extended face widths, twin-screw configurations, and custom bore sizes above 60 mm. Supply your engineering drawing for a precise quotation.
The GBC-SCS50 aluminum clamp-type shaft collar fits 50 mm bore shafts. OD 85 mm, face width 22 mm, M10 screw, 3 mm wide slot for field assembly ease, optional 14 mm keyway. Purpose-built for large industrial pump drive shafts, rolling mill pass-line rollers, and paper machine press-section roll stubs.
MOQ: 50 pcs. Minimum order value USD 1,500; mixed orders and trial quantities welcome.
Related products
-
GBC-SCS22 Aluminum Clamp Type Shaft Collar – 22mm Bore
-
GBC-SCS30 Aluminum Clamp Type Shaft Collar – 30mm Bore
-
GBC-SCS14 Aluminum Clamp Type Shaft Collar – 14mm Bore
-
GBC-SCS13 Aluminum Clamp Type Shaft Collar – 13mm Bore
-
GBC-SCS40 Aluminum Clamp Type Shaft Collar – 40mm Bore
-
GBC-SCS12 Aluminum Clamp Type Shaft Collar – 12mm Bore