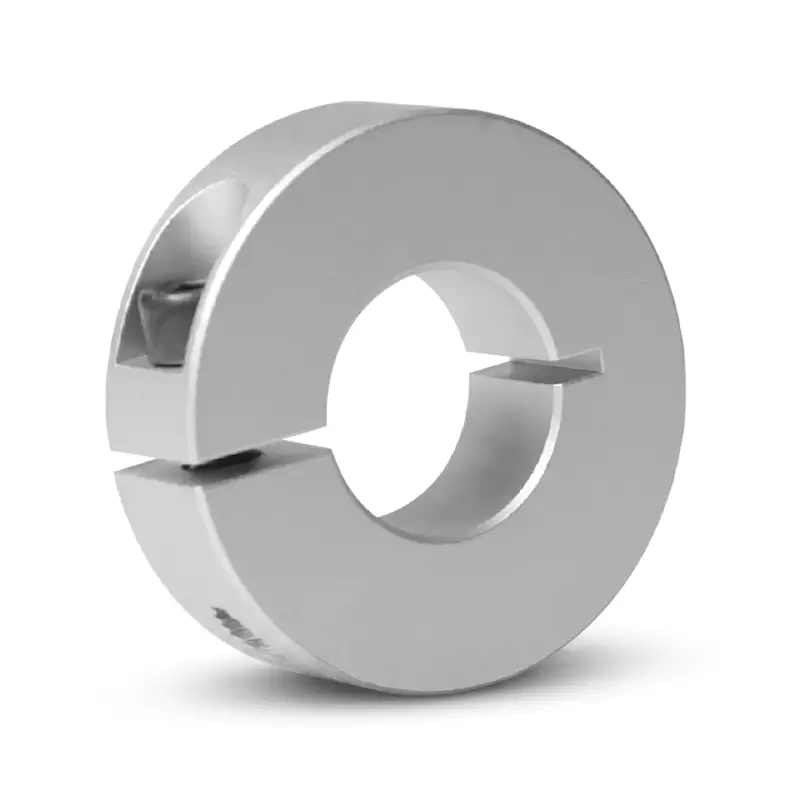
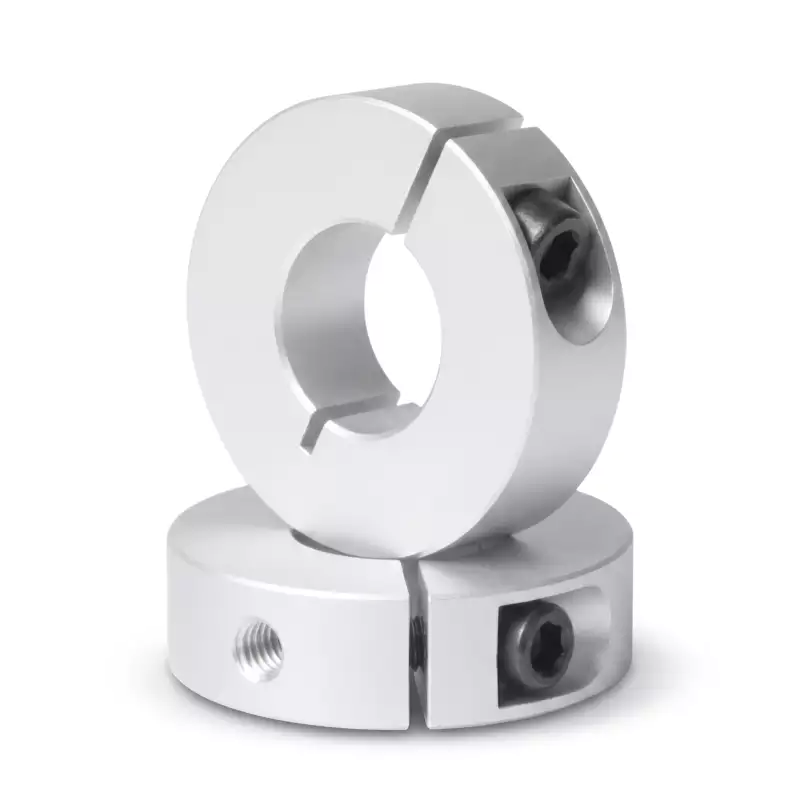
GBC-SCS60 Aluminum Clamp Type Shaft Collar – 60mm Bore
The GBC-SCS60 is the series-maximum aluminum clamp-type shaft collar for 60 mm bore shafts. OD 95 mm, face width 22 mm, M10 screw, 3 mm wide slot, optional 18 mm keyway. The definitive choice for large crushing and milling equipment, mining winch drum drives, and rotary kiln gearbox output shaft location in heavy industry.
MOQ: 50 pcs. Minimum order value USD 1,500; mixed orders and trial quantities welcome.
60mm Bore Aluminum Clamp Shaft Collar – Series Maximum, 95mm OD & 18mm Keyway for Heavy Machine Main Shafts
| Parameter | Value | Note |
|---|---|---|
| SKU / Model | GBC-SCS60 | GBC SCS Series — Large Bore |
| Bore Diameter (d) | 60 mm | Shaft h6 tolerance: 60.000 / 59.981 mm |
| Outer Diameter (D) | 95 mm | Provides thick wall for high-clamp loads |
| Face Width (B) | 22 mm | Extended width for high axial bearing area |
| Clamping Screw | M10 socket-head cap screw | Torque: 30–35 N·m · 10 mm hex key |
| Slot Width (W) | 3.0 mm | Wide slot for easy assembly over shaft features |
| Keyway Width (K) | 18 mm | DIN 6885 Form A; plain bore is default supply |
| Recommended Torque | 30–35 N·m | Use calibrated torque wrench |
| Material | Aluminium alloy | Hard-anodize, electroless nickel & steel variants available |
| MOQ | 100 pcs | Custom engineering drawings accepted |
Product Overview
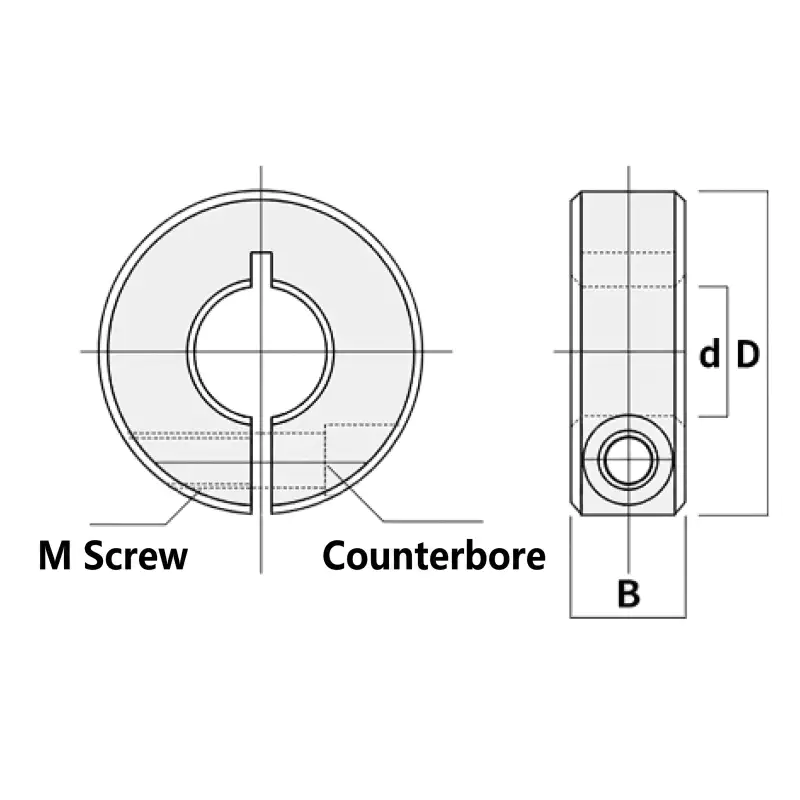
The GBC-SCS60 is the largest and most capable collar in the SCS aluminium series, consolidating every dimensional advantage accumulated across the range: 60 mm bore, 95 mm OD, 22 mm face width, M10 clamping screw at 30–35 N·m, a 3 mm wide slot for unrestricted assembly access, and an 18 mm keyway — the widest DIN 6885 key section for 60 mm bore, capable of transmitting the full rated torque of motors up to approximately 45 kW at 1,500 rpm through the key joint alone. The 95 mm OD provides the wall thickness needed to contain the M10 bore and the 18 mm keyway without compromising radial stiffness, while the 3 mm slot makes it straightforward to mount the collar over the large shaft features — wide keyways, locking-ring grooves, and thread run-outs — that are invariably present on shafts of this diameter. Applications at the 60 mm bore level are uniformly heavy: main shaft assemblies in large crushing and milling equipment, drum drives in high-capacity winch and hoist systems used in mining and marine lifting, and the output shaft location collars for large helical-bevel and planetary gearboxes driving conveyor systems, ball mills, and rotary kilns in the cement, mining, and minerals-processing industries.
Key Features
Non-Damaging Clamp Design
Circumferential clamping force eliminates shaft surface indentation, preserving ground shaft finishes and protecting adjacent seals and bearings from the accelerated wear caused by the stress-concentration marks that set-screw collars leave on large-diameter shafts where replacement cost is high.
M10 High-Capacity Clamping Screw
The M10 socket-head cap screw delivers clamping torque up to 30–35 N·m — the highest in the SCS range at this bore level — producing axial holding forces that match the sustained thrust loads of large industrial machinery operating continuously at rated capacity.
3.0 mm Wide Slot — Field Assembly Advantage
The 3.0 mm slot width provides generous bore clearance for sliding the collar over shaft keyways, threads, and groove features without tools or force — a significant advantage on large shaft assemblies built in the field without alignment fixtures or heating equipment.
22 mm Face Width — Maximum Axial Bearing Area
The 22 mm face width is matched to the bore and OD at this size to deliver the highest axial bearing area in the SCS range, distributing clamping contact pressure across a wide band that maximises holding force and minimises bore surface pressure under long-term sustained axial loads.
18 mm DIN 6885 Keyway — Full-Torque Locking Option
The 18 mm keyway follows DIN 6885 Form A for 60 mm bore, providing both axial location and full-rated rotational torque transmission through a single component. Specify at order — default supply is plain bore without keyway.
Typical Application Scenarios
Large Crushing & Milling Equipment Main Shafts
Jaw crushers, cone crushers, and ball mill pinion shafts in quarrying and minerals-processing plants operate at 60 mm as a standard shaft journal for the 18.5–37 kW drive class. The SCS60 locates drive-sprocket and coupling-hub positions on these shafts under the extreme impact loads of hard-rock crushing — loads that would cause lighter or lower-clamp collars to migrate within hours, misaligning the crusher drive and triggering overload trips.
Mining & Marine Winch Drum Drive Shafts
High-capacity winch and hoist drum drives in underground mining and marine crane applications route main drive torque through 60 mm shafts at the drum gearbox output. The SCS60 with 18 mm keyway provides the positive rotational lock and axial location that safety regulations in these sectors require — a friction-only clamp collar is insufficient where load drops due to collar slip are a safety hazard.
Rotary Kiln & Ball Mill Gearbox Output Shafts
Large helical-bevel and planetary gearboxes driving rotary kilns, ball mills, and vertical roller mills in cement and minerals production output through 60 mm journals in split-plummer-block bearings. The SCS60 locates coupling hubs at these output shafts, maintaining the sub-millimetre axial positions needed for flexible coupling element compression and the tight angular tolerances required to protect the gearbox output bearings from combined axial and radial overloads during thermal expansion of the kiln or mill shell.
Dimensional Guide & Shaft Fit Specification
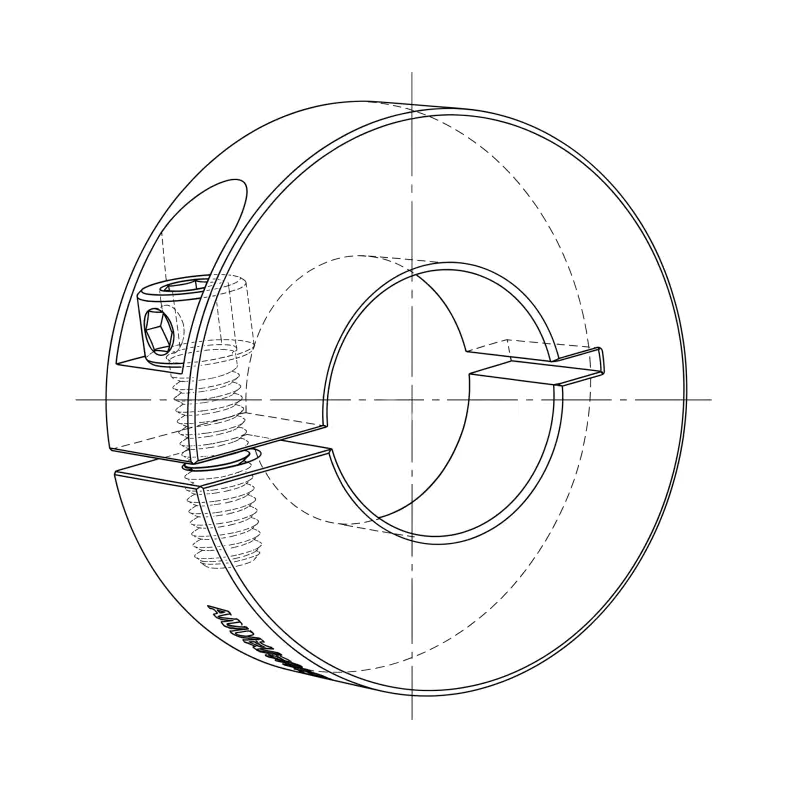
The GBC-SCS60 is defined by bore d = 60 mm, outer diameter D = 95 mm, and face width B = 22 mm. The 3.0 mm slot runs the full face width, providing the radial flex gap that allows the bore to close around the shaft as the M10 screw is tightened to 30–35 N·m. Specify the mating shaft to ISO 286 h6 (60.000 / 59.981 mm) for the optimal pre-installation sliding fit and maximum post-clamping axial retention force. Bore sizes above 40 mm must be verified with a calibrated bore gauge rather than relying on nominal dimensions — manufacturing tolerances on large shafts can approach 0.05 mm and will significantly affect clamping performance if outside the h6 band.
GBC supplies custom configurations including steel and stainless steel construction, extended face widths, twin-screw clamping, marine-grade anodizing, and bore sizes above 60 mm. Contact the GBC team via the enquiry page with your engineering drawing and application details for a tailored quotation.
Model Selection Guide
For 50 mm bore large pump and rolling-mill applications, the GBC-SCS50 provides the same M10 screw and 22 mm face width with a 14 mm keyway. The SCS60 is the top of the standard aluminium SCS range — for bore sizes above 60 mm or for applications requiring steel construction at any bore size, contact GBC to discuss custom-specification options.
| Model | Bore | Relation |
|---|---|---|
| GBC-SCS50 | 50mm | ← Smaller |
| GBC-SCS60 | 60 mm | ◀ Current |
Installation Procedure
- Shaft measurement: Measure the shaft diameter at the collar location using a calibrated micrometer or bore gauge, confirming the dimension falls within ISO h6 (60.000 / 59.981 mm). At large bore sizes, do not assume nominal dimensions — verify physically.
- Surface preparation: Degrease the clamping zone with a solvent wipe. For shafts with light rust or scale, polish with 400-grit abrasive cloth before degreasing. Remove all burrs from keyway edges to prevent bore scoring during collar installation.
- Collar positioning: Open the slot fully by backing off the M10 screw two full turns. Slide the GBC-SCS60 onto the shaft to the required position, referencing a pre-set depth gauge or spacer for repeatable placement. Torque M10 screw to 32–35 N·m using a calibrated torque wrench with an 8 mm hex-bit socket. Verify shaft h6 tolerance ({bore}.000 / 59.981 mm) with a bore gauge before installation — at 60 mm bore, even a 0.05 mm oversize shaft will prevent the collar from seating correctly and must be corrected before clamping.
- Torqued clamping: Using a calibrated torque wrench with a 10 mm hex-bit socket, tighten the M10 screw in three steps — 30%, 70%, then 30–35 N·m — checking position after each step. Mark the screw head with a paint pen after final tightening to detect any self-loosening during subsequent inspections.
Frequently Asked Questions
What is the maximum axial force the SCS60 can hold, and how does it compare to a machined locking collar?
How do I prevent the 3mm slot from becoming a contamination ingress path in a cement plant environment?
Can the SCS60 18mm keyway transmit the full rated output torque of a 37kW gearbox?
Related Products
Browse adjacent sizes and associated shaft components from GBC:
- GBC-SCS50 – 50mm bore aluminum clamp shaft collar — next smaller size in the heavy-bore SCS range
- Complete GBC SCS Shaft Collar Series — all standard bore sizes from 6 mm to 60 mm, with custom options beyond
Request a Quote or Discuss a Custom Specification
Minimum order quantity is 100 pcs. GBC supplies steel and stainless steel variants, marine-grade hard-anodizing, extended face widths, twin-screw configurations, and custom bore sizes above 60 mm. Supply your engineering drawing for a precise quotation.
The GBC-SCS60 is the series-maximum aluminum clamp-type shaft collar for 60 mm bore shafts. OD 95 mm, face width 22 mm, M10 screw, 3 mm wide slot, optional 18 mm keyway. The definitive choice for large crushing and milling equipment, mining winch drum drives, and rotary kiln gearbox output shaft location in heavy industry.
MOQ: 50 pcs. Minimum order value USD 1,500; mixed orders and trial quantities welcome.
Related products
-
GBC-SCS50 Aluminum Clamp Type Shaft Collar – 50mm Bore
-
GBC-SCS08 Aluminum Clamp Type Shaft Collar – 8mm Bore
-
GBC-SCS16 Aluminum Clamp Type Shaft Collar – 16mm Bore
-
GBC-SCS20 Aluminum Clamp Type Shaft Collar – 20mm Bore
-
GBC-SCS35 Aluminum Clamp Type Shaft Collar – 35mm Bore
-
GBC-SCS06 Aluminum Clamp Type Shaft Collar – 6mm Bore