UKFC200+H Series Flange Cartridge Bearing Units
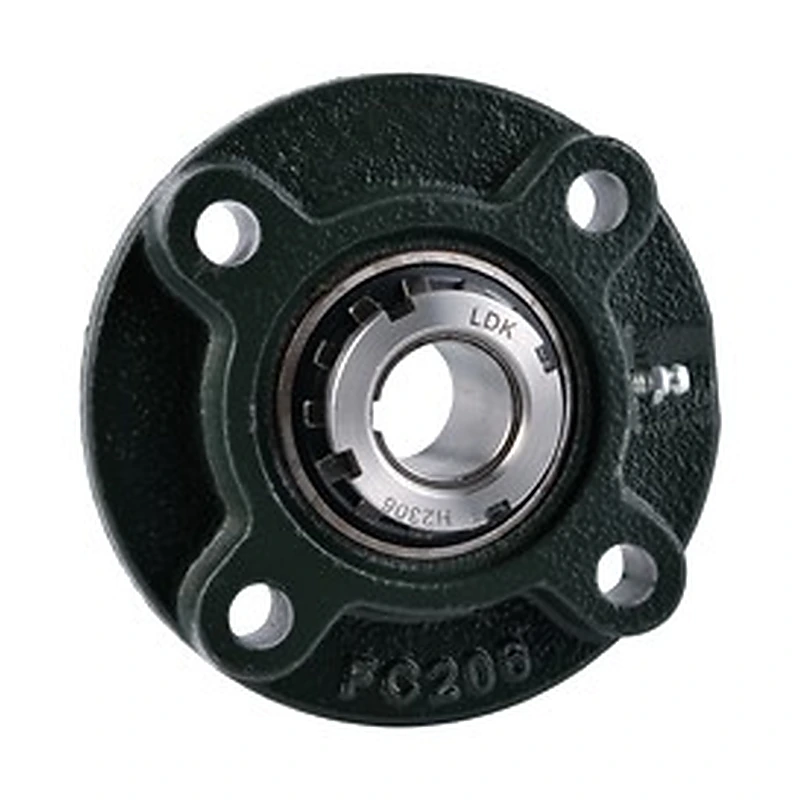
UKFC200+H should be treated as an assembly rather than as a simple bored bearing unit. The tapered-bore insert works with an H-series adapter sleeve, so the shaft, sleeve and bearing reference all belong in the selection process. That makes this family useful when an adapter-sleeve mounting arrangement is already part of the machine design.
The catalogue lists combinations from UKFC205+H2305 through UKFC218+H2318 and shows a 20-80 mm published shaft range. Because the sleeve changes the way the bearing is mounted and identified, a correct replacement needs more information than a shaft diameter and four bolt-hole measurements.
For a wider housing comparison, browse the bearings range before finalising the mounting style.
UKFC200+H published technical range
The table below keeps the catalogue values used for this series. Use the model-specific drawing for the final interchange decision; dimensions and suffixes can vary inside a family.
| Specification point | UKFC200+H catalogue data |
|---|---|
| Series / model family | UKFC205+H2305 to UKFC218+H2318 |
| Duty class | Standard duty |
| Locking / bearing mounting | Tapered bore with adapter sleeve locking |
| Published shaft range | 20-80 mm |
| Published metric / inch options | 20, 25, 30, 35, 40, 45, 50, 55, 60, 65, 70, 75, 80 mm |
| Housing / mounting style | 4-bolt round flange cartridge housing |
| Housing construction | Cast iron |
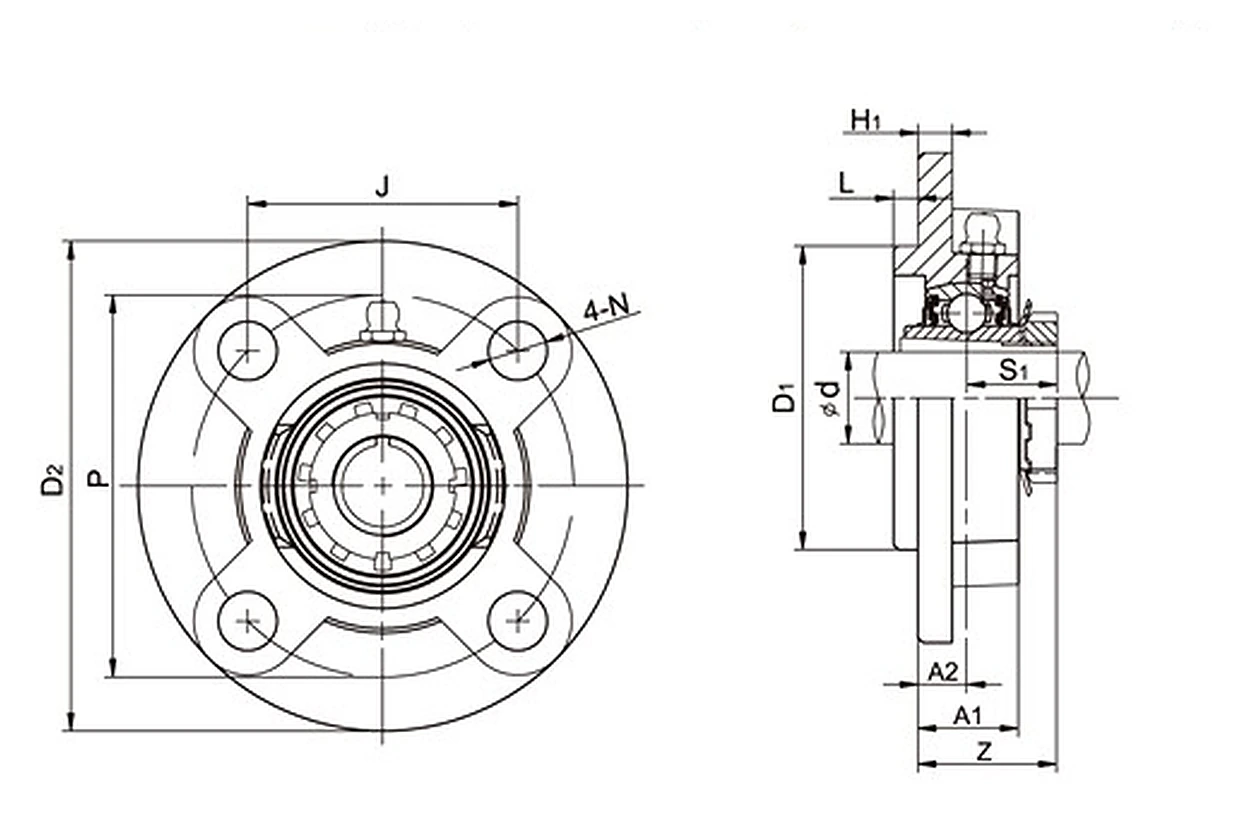
| Catalog dimensional fields | D2, P, J, A2, N, L, H1, A1, D1, S1, Z, bolt size and weight |
| Published unit weight | 0.98-13.30 kg |
Cross-checking UKFC200+H against other FC options
UKFC200+H is not a direct functional duplicate of UCFC, NAFC or UEFC simply because the housings share round four-bolt geometry. The adapter-sleeve arrangement is the defining difference. Use another FC family only when the shaft-locking method has been reviewed and approved for the machine.
Where a tapered-bore cartridge arrangement makes sense
These are application patterns where the housing concept is commonly considered. Final suitability still depends on load, speed, alignment, environment and the machine designer’s requirements.
Industrial shaft supports with sleeve-mounted bearings
Suitable where the machine specification already uses adapter sleeves to mount tapered-bore inserts.
Replacement of established UKFC+H assemblies
The clearest use case is a like-for-like service replacement where both housing and sleeve references are known.
Larger face-mounted shaft stations
The series extends to 80 mm published shaft size while retaining the round cartridge housing concept.
OEM designs that standardise sleeve components
A machine builder can keep a consistent bearing mounting method across several shaft sizes by specifying the full assembly.
Why the adapter sleeve changes the buying process
Tapered-bore bearing insert
The bearing is not simply locked directly to the shaft by radial setscrews.
Matched H-series sleeve
The adapter sleeve reference forms part of the catalogue model and should be preserved during replacement.
Round four-bolt housing
The external mounting concept remains a compact face-mounted cast-iron cartridge.
20-80 mm shaft coverage
Published shaft sizes span common medium and larger metric diameters within the listed series.
Installation depends on the sleeve as well as the housing
Store the bearing unit and matching adapter sleeve as one spare set when the machine BOM calls for the complete assembly.
Damage, contamination or corrosion can affect mounting even when the housing dimensions are correct.
Bearing internal clearance and sleeve position are installation matters; do not copy a setscrew-unit procedure.
Record the installed sleeve reference so the next maintenance cycle can order the same combination without dismantling first.
Three references to confirm before ordering
Use the product drawing as the final dimensional authority. The points below are practical filters that help narrow the correct model before a full drawing comparison.
Record both the UKFC housing/bearing reference and the H-series sleeve rather than shortening the part number.
Use the actual shaft diameter as a cross-check; do not infer it only from an old housing casting number.
Pilot, bolt-circle, housing thickness and insert position still need to match the machine face.
The installer needs enough working room for the sleeve and locking components as well as the flange bolts.
Send the machine details for a model check
For UKFC200+H, send the existing model marking, shaft diameter, mounting dimensions and a photo of the bearing position. GBC can review the information against the published series before quotation. Email: sales@australia-drive.com.